Get a quote →
44 Ilana Street, Delville, Germiston
011 383 2141 · 076 353 6592
sales@ikplus.co.za
Capabilities / Plant & envelope

Everything
we can actually do.

Every spec on this page, with nothing rounded up. What we cut, how thick, how long a bend, how much force. There is a calculator further down that you are welcome to use whether or not you ever send us a job.

  • 6 kW fibre laser
  • 160 T press brake
  • 10 T overhead crane
  • 15 kW compressor
Plant register

Every machine has
somebody's name on it.

Site Germiston
Shift Mon–Fri 07:00–17:00
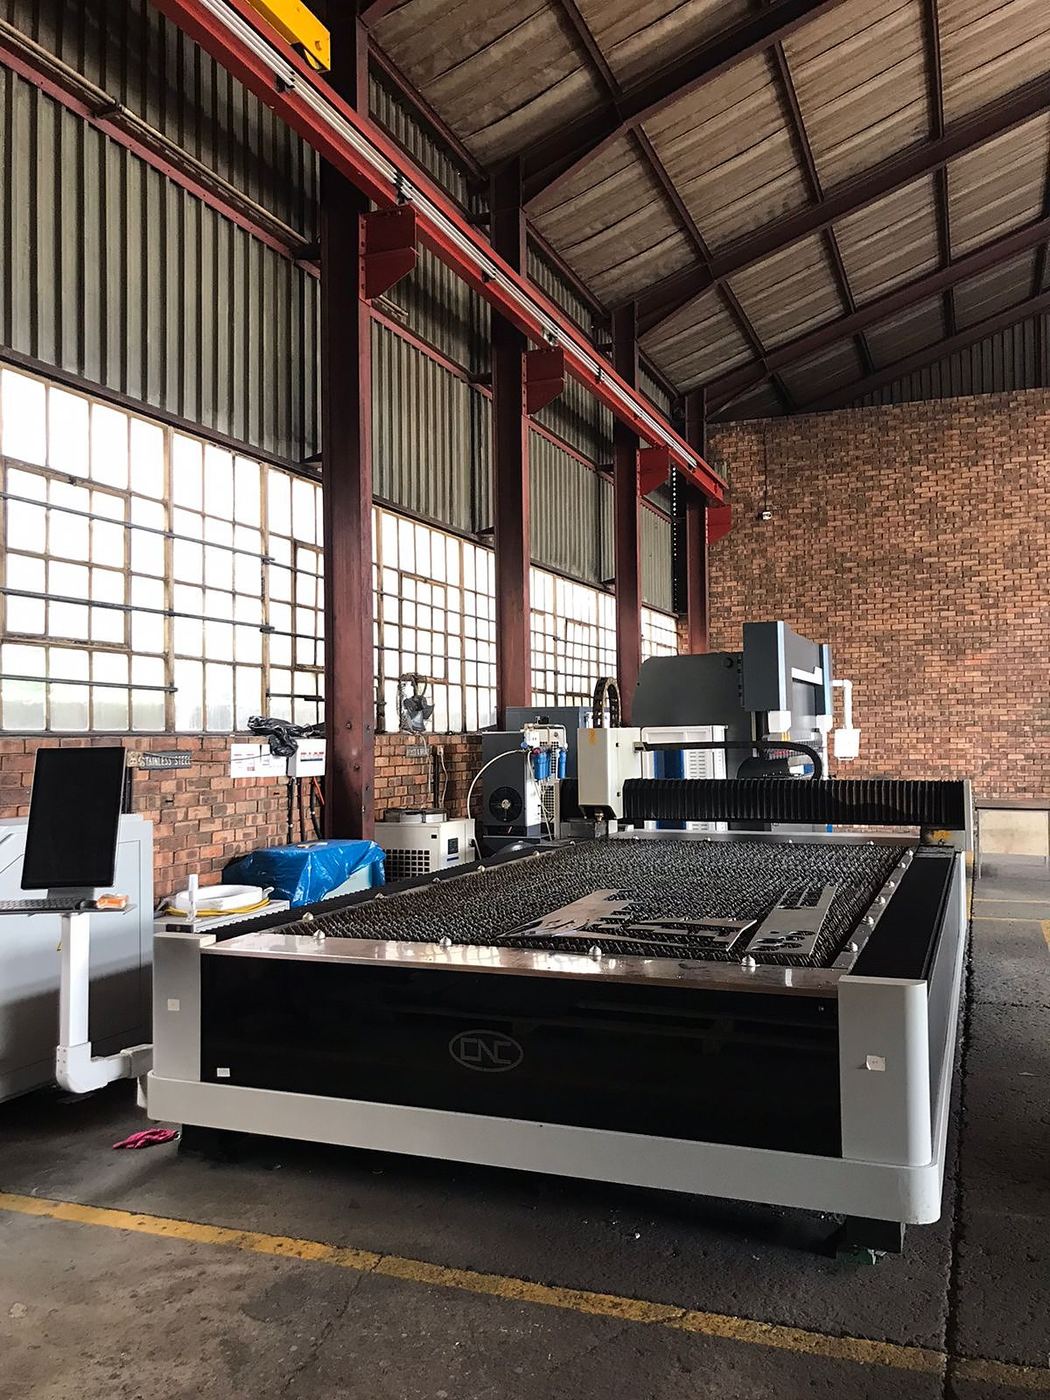
6 kW CNC fibre laser cutter
PLANT 01

6 kW CNC fibre laser cutter

Power source6 kW fibre
Bed size4000 × 2000 mm
Max thickness30 mm (material dependent)
Mild steelUp to 30 mm
Stainless steelUp to 16 mm
AluminiumUp to 12 mm
ControlPrecision cutting path, automatic height sensing
NestingCypNest / ProNest optimisation on every job
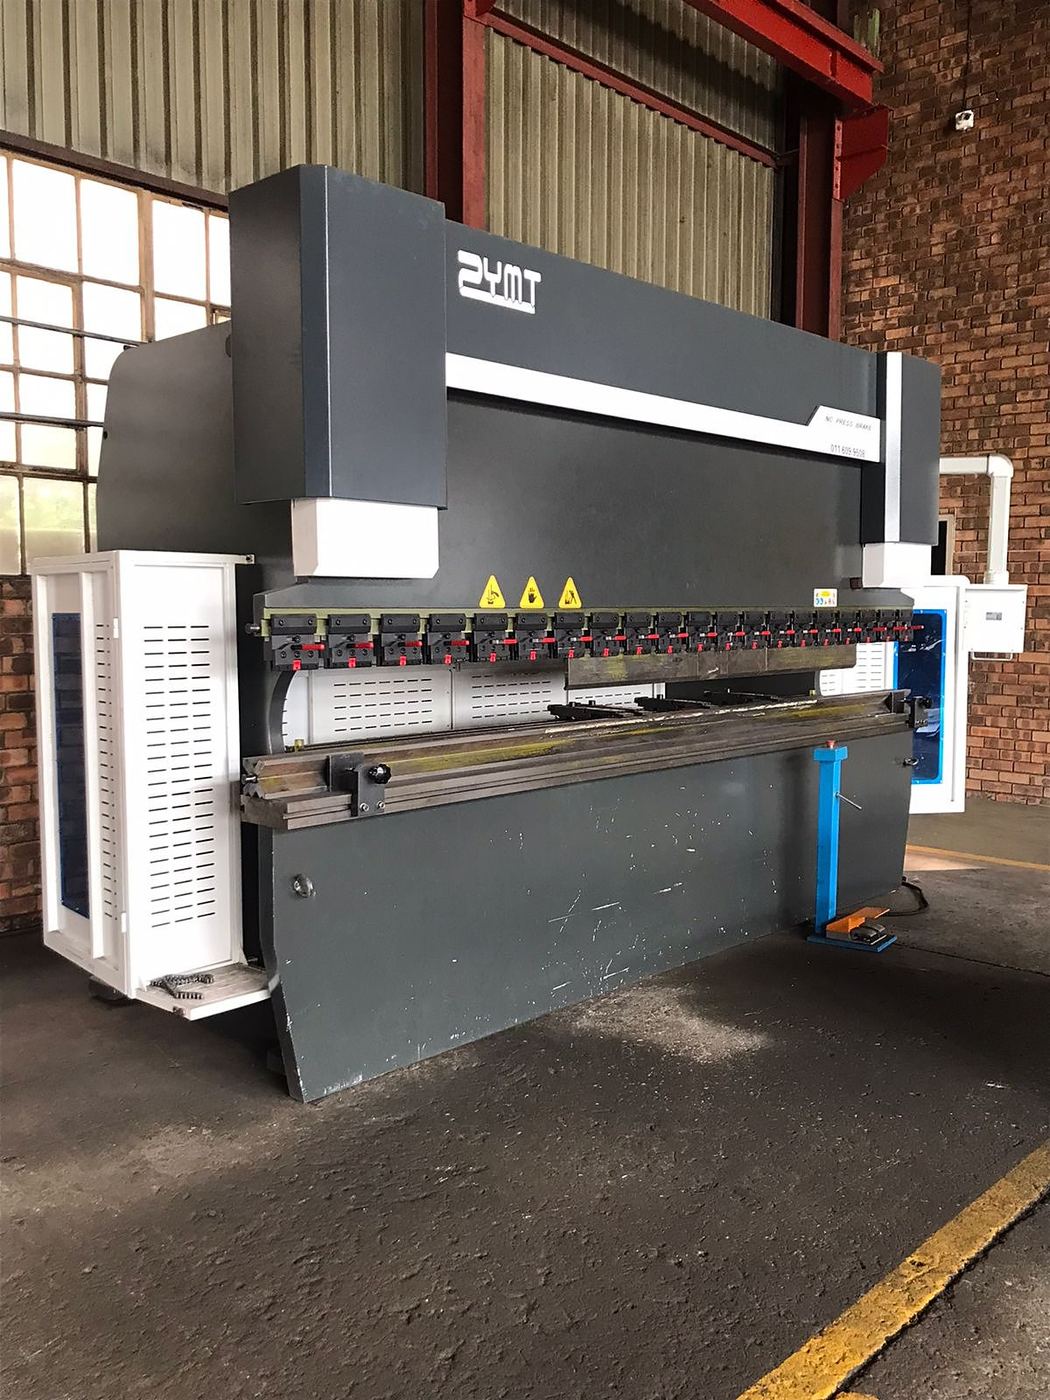
160 tonne CNC press brake
PLANT 02

160 T CNC press brake

Bending force160 tonnes
Max bend length4000 mm
ControlFully CNC with programmable back-gauge
Repeatability≈ ±0.1 mm
Bend typesMulti-stage, complex geometry, air bending
ToolingSelected per material and thickness
Typical dieV ≈ 8 × material thickness
SurfaceTooling chosen to protect the finish
PLANT 03

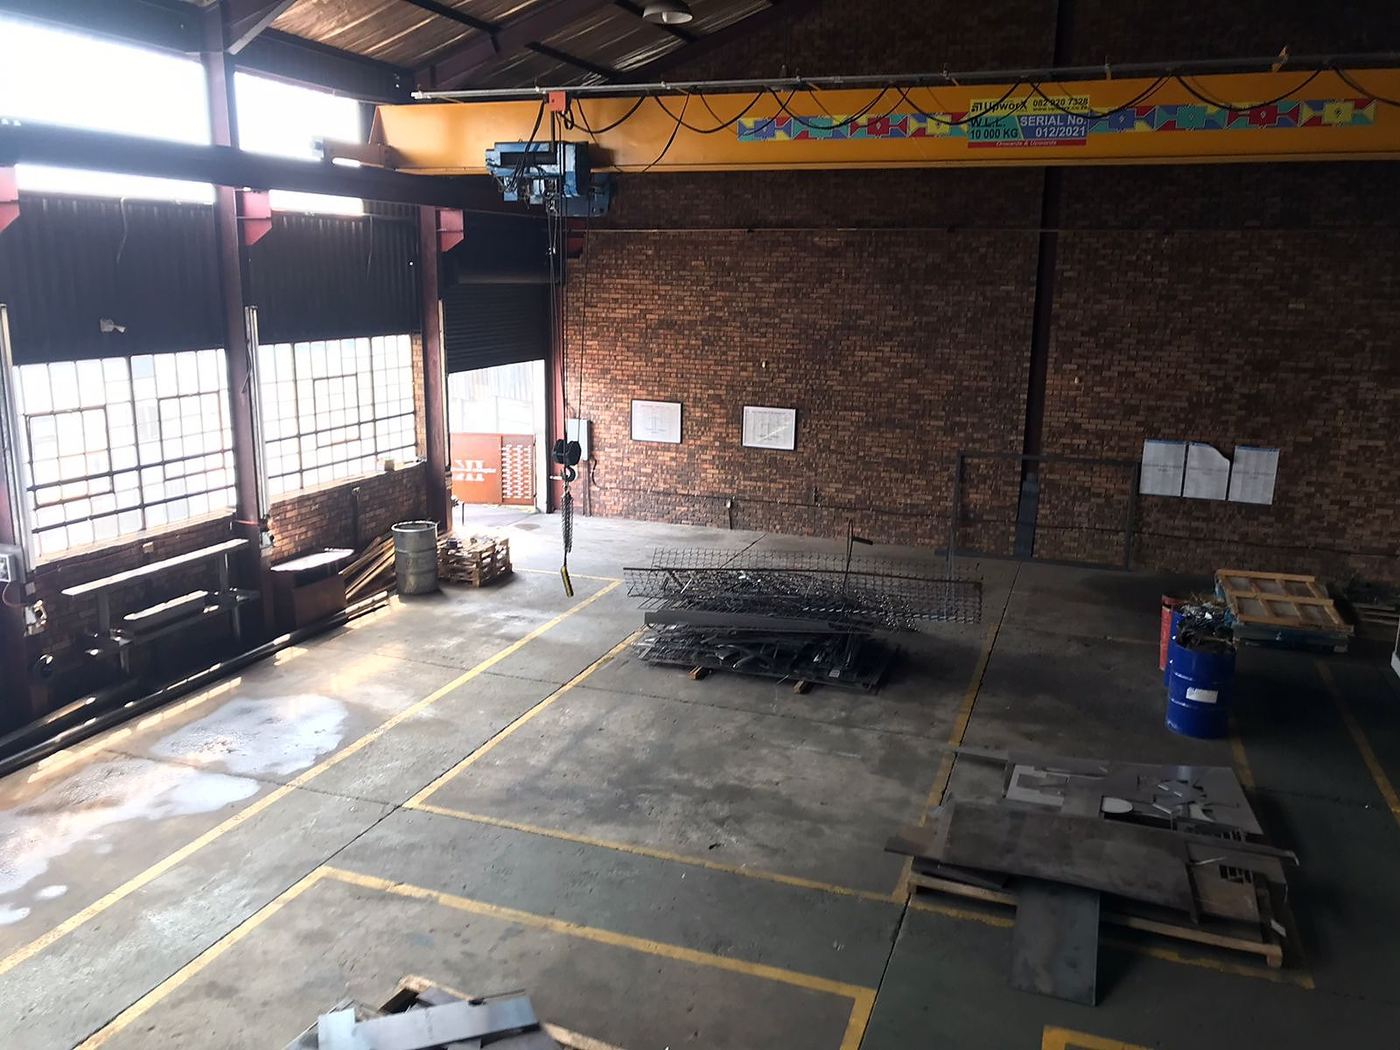
10 T overhead crane

Heavy plate and large assemblies get moved in-house. No hired lifting gear, no waiting for it to turn up.

PLANT 04

15 kW air compressor

Assist gas and shop air, sized so the laser never sits waiting for pressure.

PLANT 05

2 × 350 W CO₂ welders

Fabrication, assembly and finishing here, so weldments never leave the building.

Material envelope

What we cut,
and where it stops.

Bed 4000 × 2000 mm
Bend 4000 mm / 160 T
Material Max thickness Typical grades Notes
Mild steel30 mmS235 · S355 · plate & sheetClean edge, minimal burr through the range
Stainless steel16 mm304 · 316Nitrogen cut for an oxide-free edge on thinner gauges
Aluminium12 mm5052 · 6082Tooling selected to avoid marking the surface on bends

Thickness depends on material and grade. If your part sits right at the edge of that table, send it anyway. We will tell you honestly whether it cuts cleanly or whether you want plasma or waterjet instead.

Engineering tool

Work out your bend
before you draw it.

Method Air bending
K-factor 0.42

Tonnage, inside radius, minimum flange and bend deduction. Punch the numbers in and it will also tell you straight away whether our 160 T brake can do it. Free, no sign-up, nothing sent anywhere.

ResultAir bending
Die opening V
Force per metre
Total tonnage required
Resulting inside radius
Minimum flange
Bend allowance
Bend deduction
if it says no, phone us anyway. there is usually a way round it

Air-bending estimate using P = 1.42 · Rm · t² / V, K-factor 0.42, inside radius ≈ 0.16 · V, minimum flange ≈ 0.63 · V. Real tooling, grain direction and whatever batch the steel came from will all move these numbers a bit. Treat it as a sanity check, not gospel.

Draughting office

We work from your file,
not a redraw of it.

Your native file goes straight to production instead of getting redrawn by hand. Redrawing is where dimensions quietly change, and nobody notices until the part is on site.

AutoCAD

2D draughting and DXF preparation

Inventor

3D parametric modelling

SolidWorks

Sheet-metal models and flat patterns

CypCut

Laser machine control

CypNest

Nesting and sheet layout

ProNest

Advanced material optimisation

The facility

All of it, one roof.

Address 44 Ilana Street, Delville
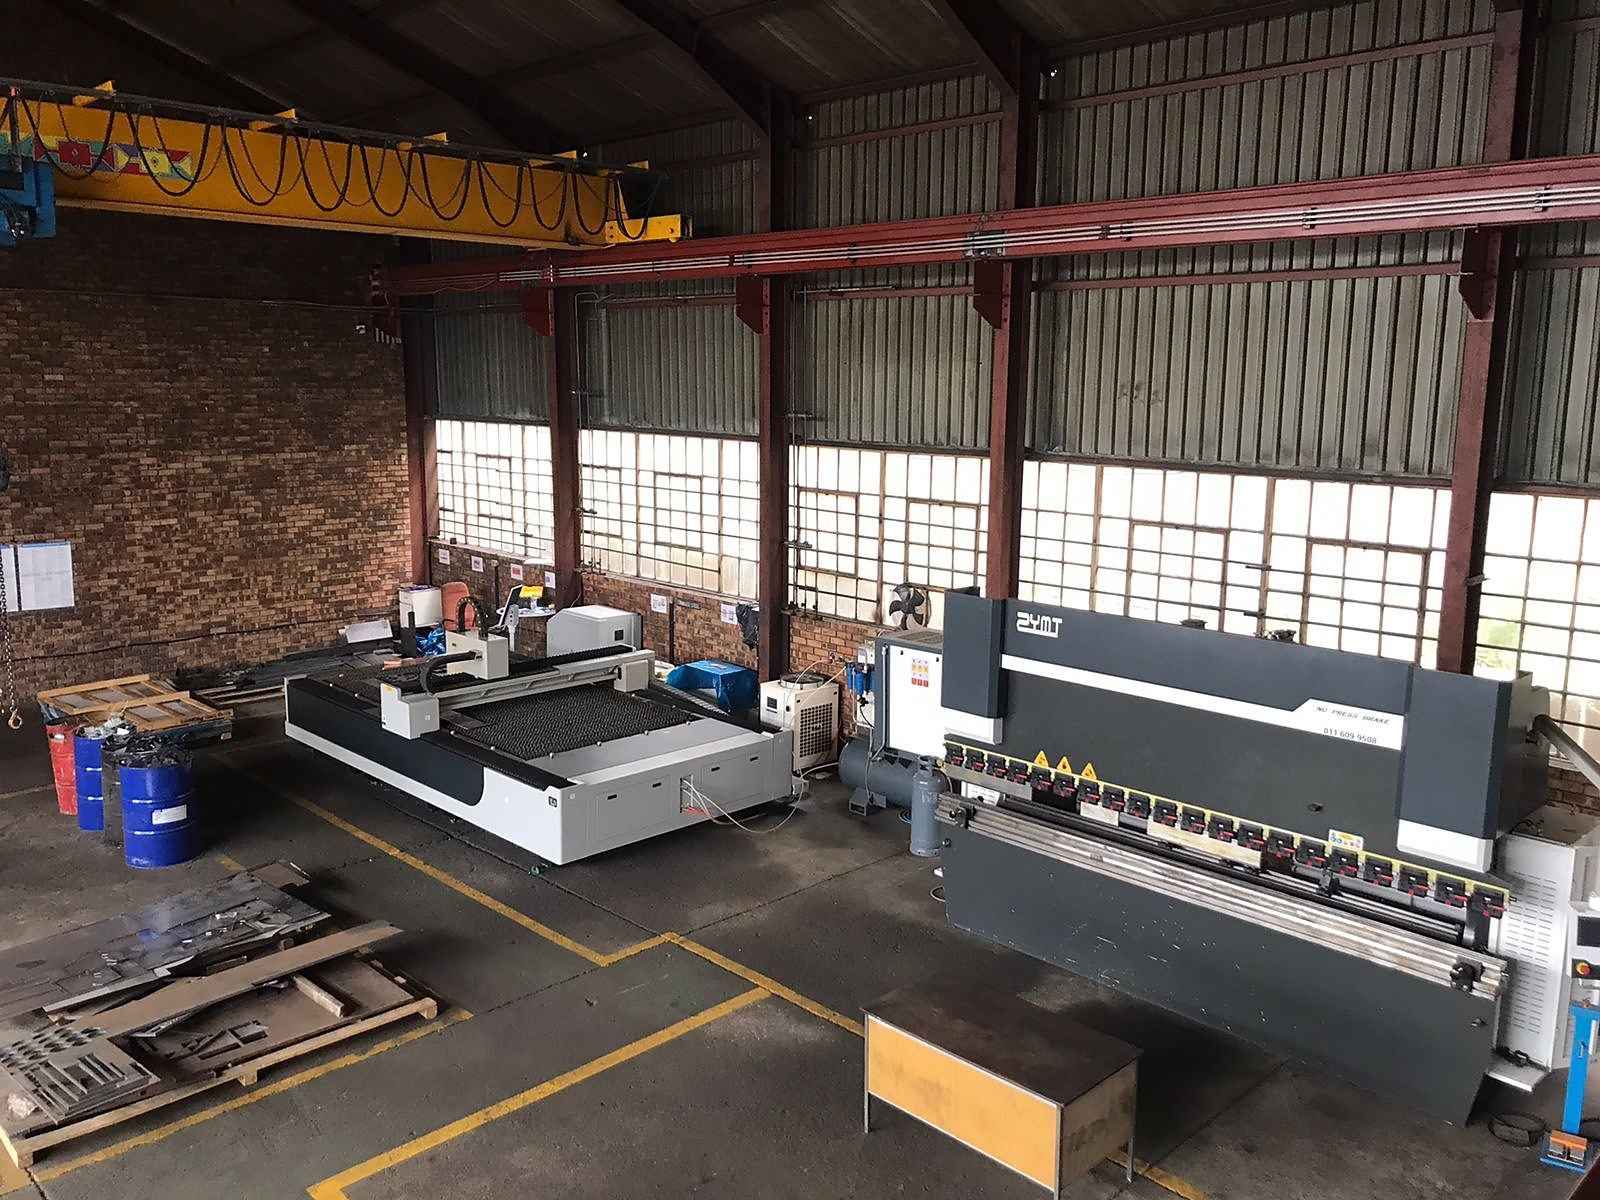
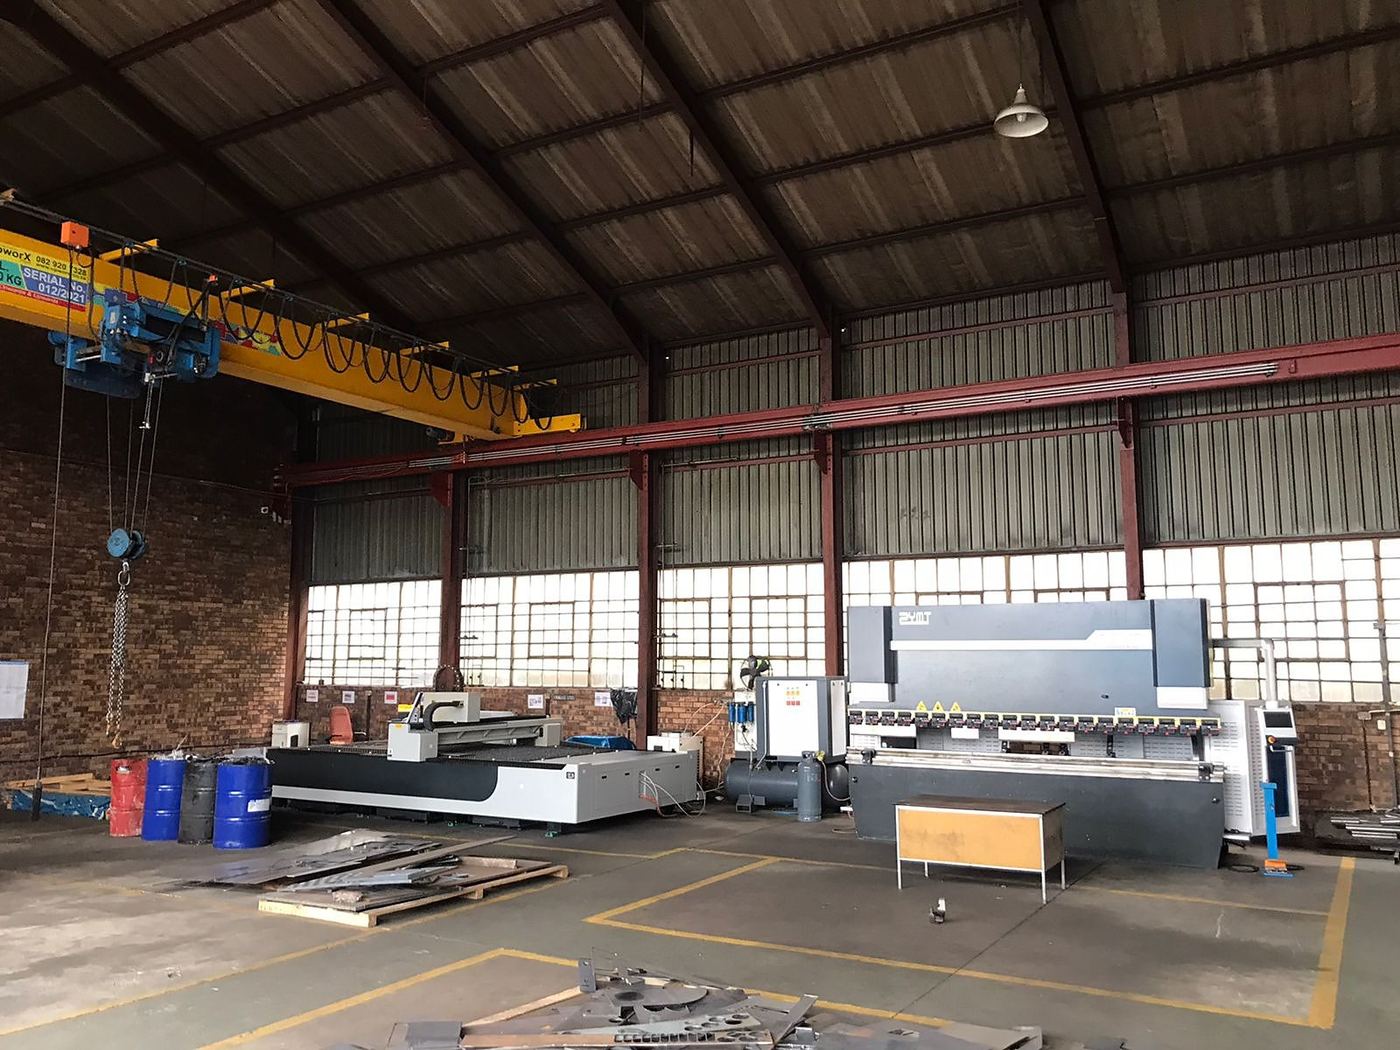
The IK Plus workshop floor with overhead crane

Workshop floor

Laser, brake, welding bays and crane, all within shouting distance.

10 tonne overhead crane above the IK Plus workshop

Material handling

10 tonnes overhead, so nothing waits for a hired crane.

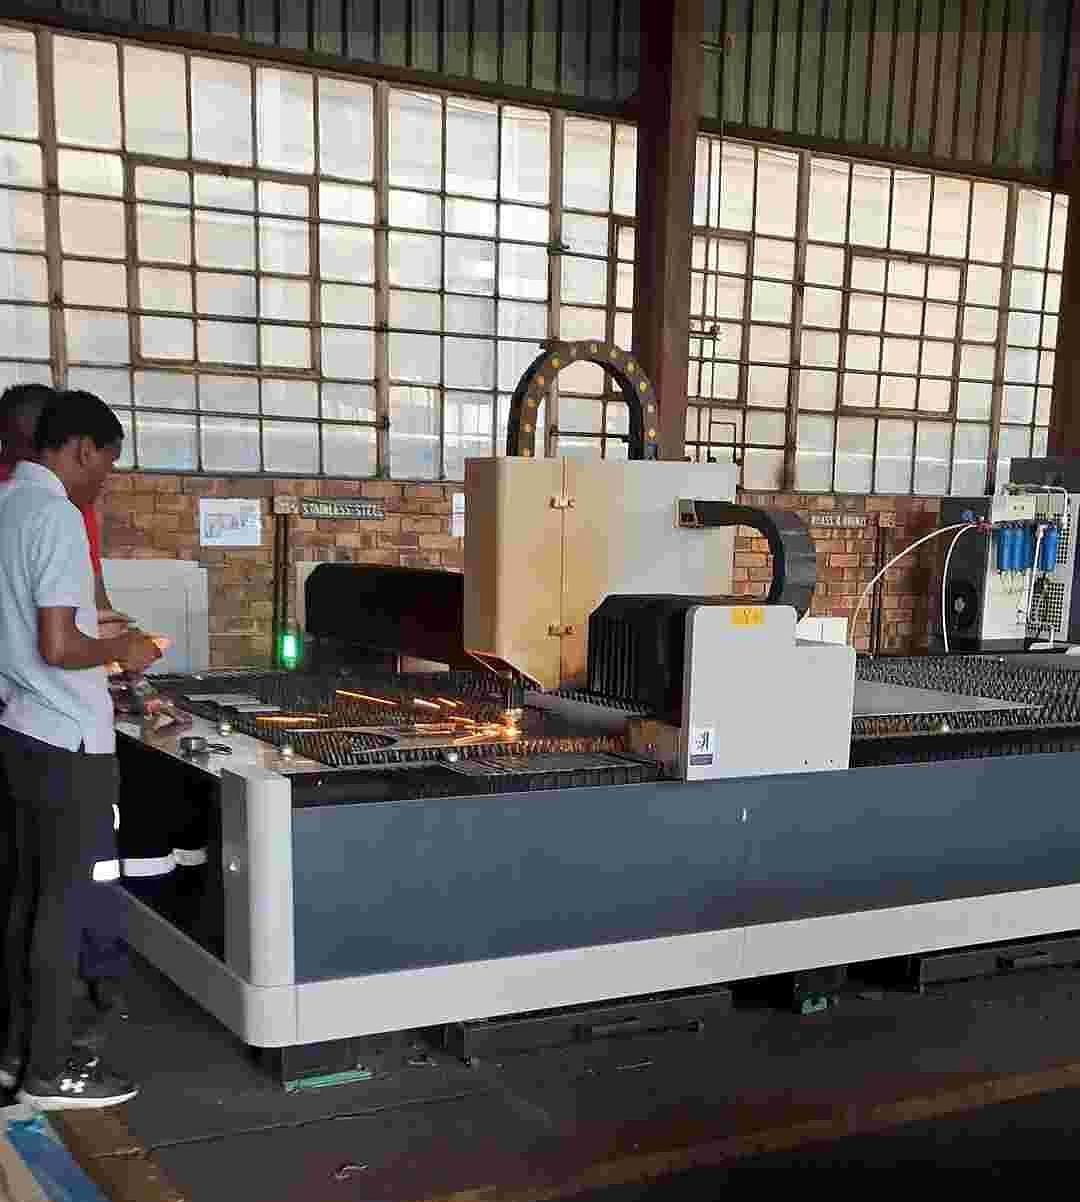
An IK Plus operator running the fibre laser

Dedicated operators

Trained technicians who stay on the same machine, not whoever is free.

Not sure your part fits?

The estimator checks size, thickness and bend force against these exact machines, and tells you before you commit to anything.